Solution
Mold Monitoring and Tooling Management
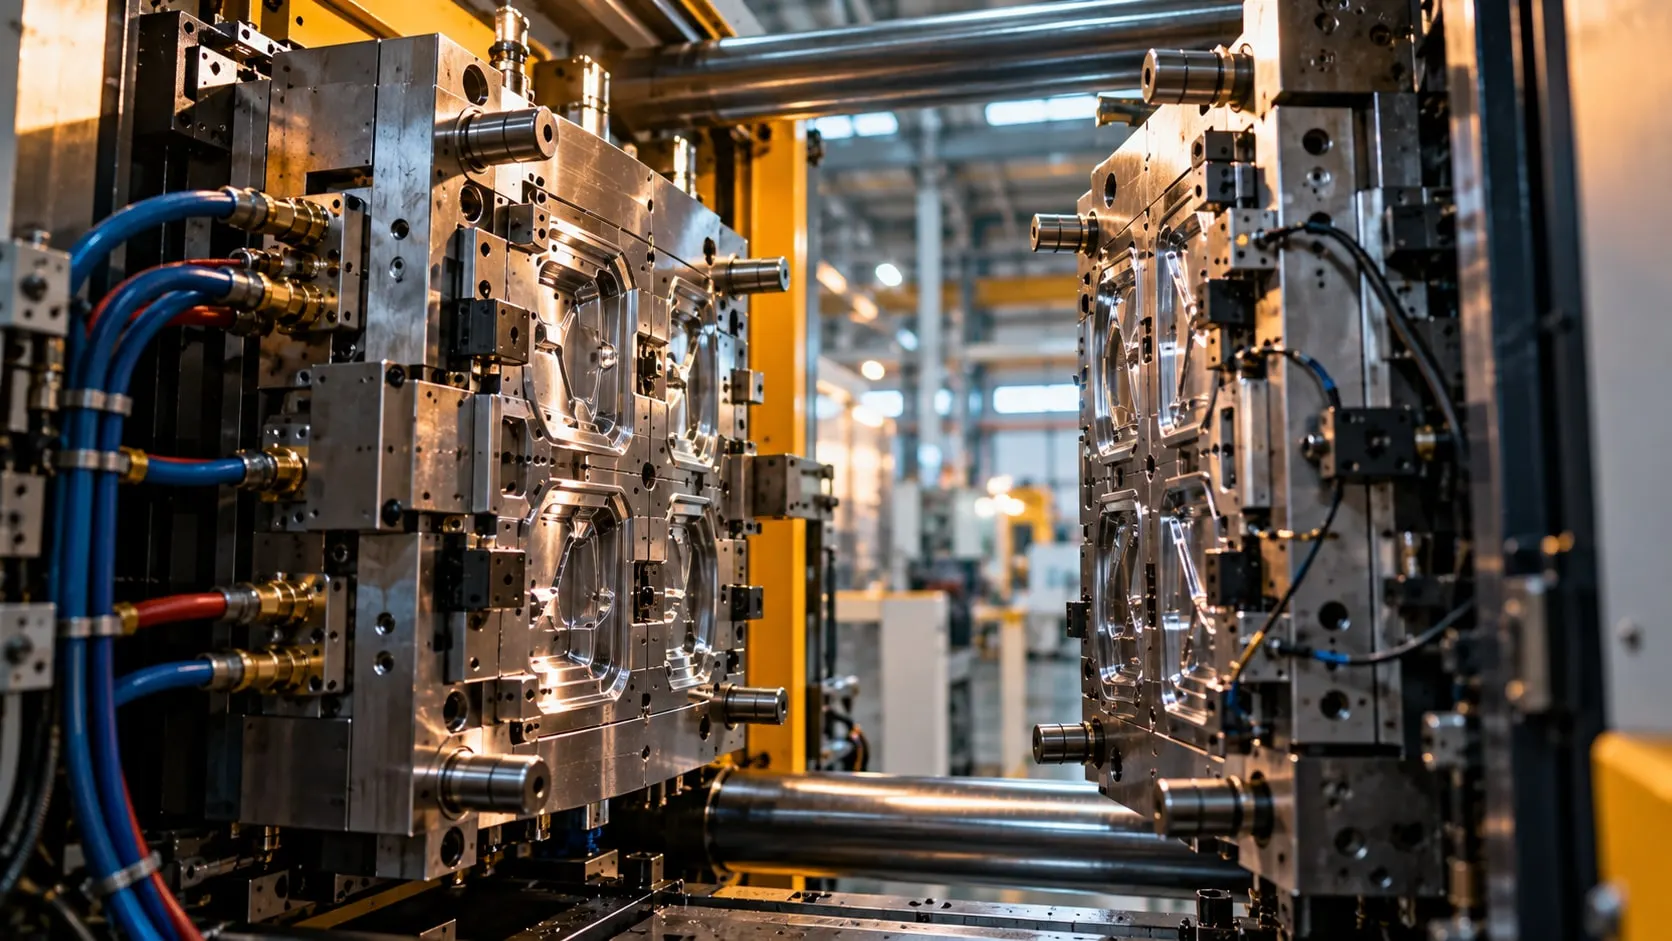
We build mold monitoring that records which mold ran on which machine and how many shots it made, and plans maintenance on actual shot counts.
Our clients
- Siemens
- Anadolu Isuzu
- BSH
- Tofaş
- Toyotetsu
- Martur
- Turkcell
- Vodafone
- Doğadan
- Pakmaya
- Bross
- Abdi İbrahim
- Nobel İlaç
- Plastimak
- Dalgıç Kalıp
- Barbaros Motor
- Magneti Marelli
- Rözmaş
- Sanel
A mold monitoring system tracks which mold runs on which machine, how many shots it has made and when it is due for maintenance. In injection molding, stamping and die casting, molds and dies are among the most expensive assets, yet shot counts are often written on a card. When a mold moves to another machine the count is lost, and maintenance happens either too early or after flash and dimensional problems appear.
VOLSOFT takes shot and cycle data straight from the machine: controller interfaces, OPC UA or Euromap-based interfaces on injection molding machines, PLC counters on presses. Which mold is mounted comes from the mold number in the machine, the operator terminal or a barcode or RFID read.
Because mold data lives on the same Proxus foundation as production monitoring, OEE, cycle time and scrap rate are also visible per mold.
What we deliver
Mold Monitoring
-
Automatic shot counter
Every shot is read from the machine and booked to the mold mounted at that moment, and the lifetime count travels with the mold between machines.
-
Mold-to-machine history
Which machine a mold ran on, when, and for which work orders is recorded automatically.
-
Shot-based maintenance
Each mold gets a preventive maintenance interval in shots, and the toolroom and planners are alerted as it approaches.
-
Cycle time and cavitation
Actual cycle time per mold is compared with standard, and blocked cavities are reflected correctly in part counts.
-
Changeover time
Mold change times are measured, giving SMED work real data instead of stopwatch samples.
How a project runs
From discovery to live, step by step
- 01
Mold inventory
Molds, cavity counts, standard cycle times and current maintenance intervals are collected with the toolroom.
- 02
Machine connectivity
Shot and cycle signals are read from injection, press or casting machines, and the mold identification method is chosen.
- 03
Rules and alerts
Rules for shot-based maintenance limits, cycle deviations and changeover logging are configured.
- 04
Dashboards and training
Views for the toolroom, planning and production go live and the paper mold card is retired.
Built on Proxus
Shot signals are counted at the Proxus edge and booked to the mounted mold; if the network drops, no shots are lost and they are forwarded once the link returns.
Proxus is the industrial data platform built by the VOLSOFT team.
Frequently asked questions
Common questions
What is a mold monitoring system?
A mold monitoring system automatically tracks which machine each mold runs on, its lifetime shot count, cycle time and maintenance due date. It replaces paper mold cards with data taken directly from the machines.
How do you track mold shot counts automatically?
Shot counts are read from the machine controller, an OPC UA or Euromap-based interface, or the cycle signal in the PLC. Each shot is booked to the mold mounted at that moment, so the lifetime count stays correct when the mold changes machines.
When should mold maintenance be done?
Mold maintenance should follow shot-count intervals defined by the moldmaker and your toolroom, not the calendar. Rising cycle time and scrap rate can signal that maintenance is needed earlier.
How does the system know which mold is mounted?
Many injection molding machines expose a mold or recipe number in the controller. Where they do not, operators select the mold on a terminal or scan a barcode or RFID tag. The method is chosen to fit your machine park.
Does it work for stamping dies and die casting?
Yes. On presses and die-casting machines the stroke or shot signal comes from the PLC and is booked to the die the same way. The tracked asset can be a mold, a die or a fixture.
Related pages
Often looked at together
- ServiceMES and OEE ImplementationProduction tracking with automatic OEE, downtime, work orders and shift reports from machine data.Explore→
- ServiceMachine Data CollectionRead-only production data collection from PLCs, CNCs and robots, with control logic left untouched.Explore→
- IndustryPlastics and injection moldingCycle time, mold changes, scrap and OEE tracking across injection molding machines.Explore→
- IndustryAutomotiveData collection on press, welding and assembly lines, IATF 16949 traceability and OEE.Explore→
- TechnologyOPC UA integrationConnecting to OPC UA servers with security modes and certificates, node selection and data modeling.Explore→
Next step
Let’s turn your goal into a clear engineering scope.
Tell us about your plant, your machines and your goal. An integration engineer will set up a discovery call with you.