Industry
Production data, coil tracking and energy monitoring for metal and steel processing
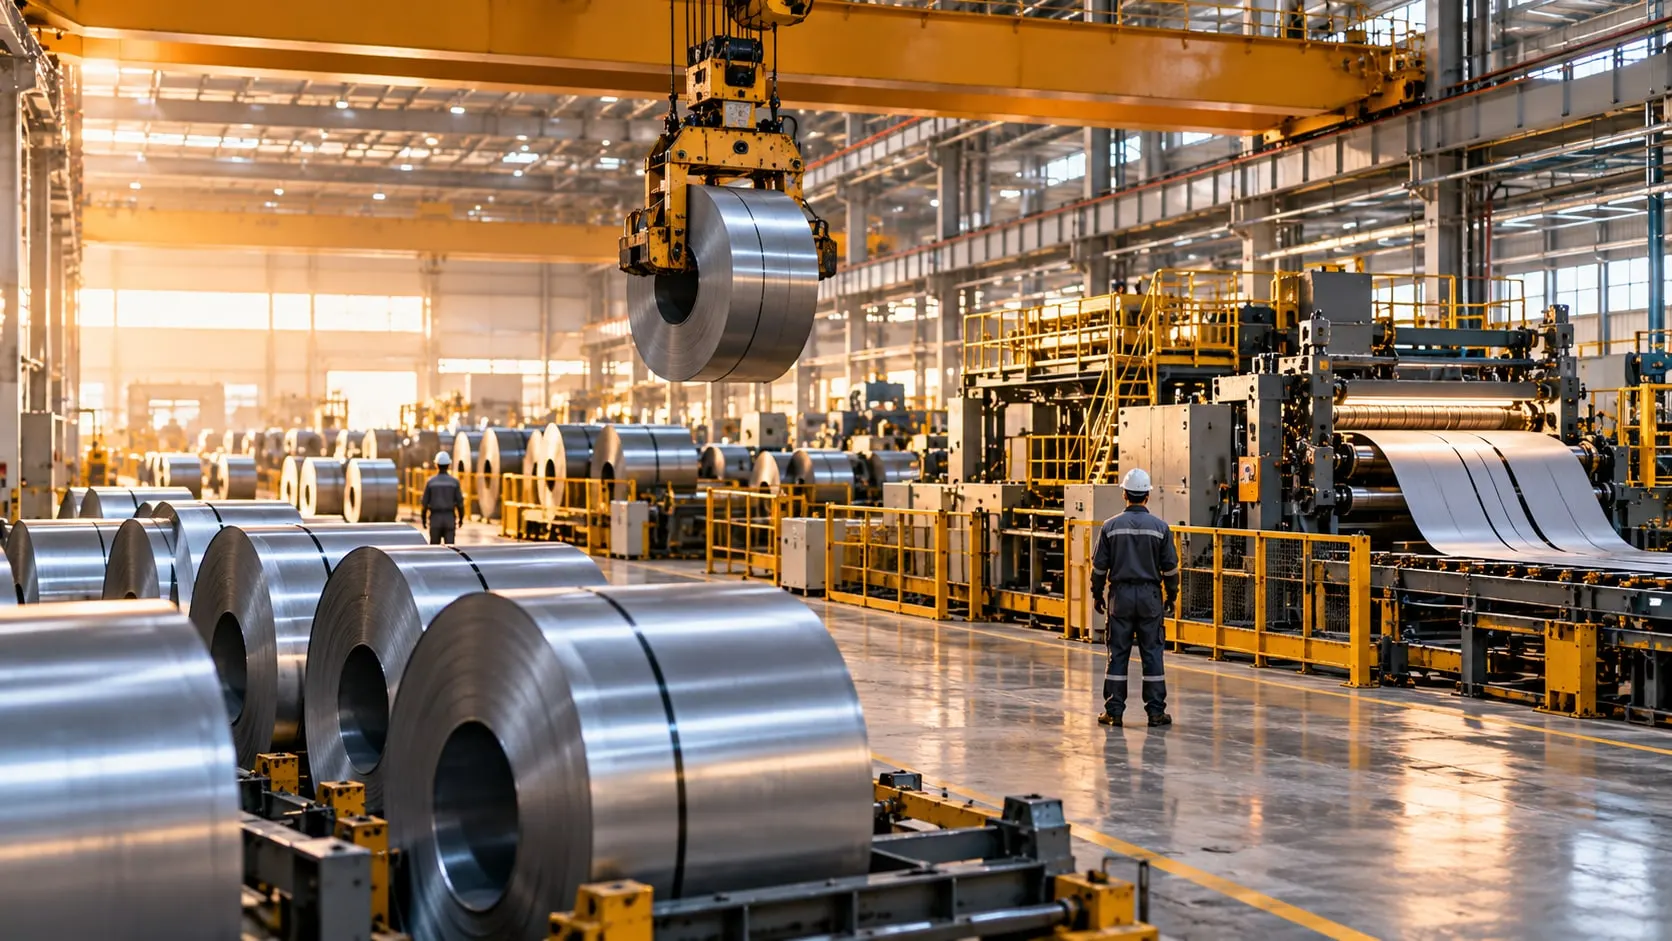
We take speed, length, weight and downtime data from slitting, cut-to-length, rolling and tube lines and report it per coil, together with energy use.
Our clients
- Siemens
- Anadolu Isuzu
- BSH
- Tofaş
- Toyotetsu
- Martur
- Turkcell
- Vodafone
- Doğadan
- Pakmaya
- Bross
- Abdi İbrahim
- Nobel İlaç
- Plastimak
- Dalgıç Kalıp
- Barbaros Motor
- Magneti Marelli
- Rözmaş
- Sanel
Metal and steel processing tracks material as weighed coils, sheets and bundles, and losses tend to hide in coil changes, setup time and head, tail and edge scrap. The line PLC knows speed and length, the scale knows weight and the ERP knows the order, but the three are rarely connected.
VOLSOFT reads speed, length, tension, downtime and alarm data from line PLCs and drives without touching control logic, and takes weights from scales and weighbridges. The data is matched with the input coil, the output bundle and the work order.
You can then see which bundles came from which coil, how much scrap was produced and how much energy the line used, in the same record. Energy loads are high in heavy industry, so energy monitoring is part of most projects. Every project runs on Proxus.
What we deliver
Metal and steel
-
Coil and bundle traceability
The input coil's number, grade and weight are matched with the output bundles and strips. Label and weighing data are linked to the work order.
-
Line speed, length and downtime
Speed, length and stoppages are read from the PLCs of slitting, cut-to-length and rolling lines. Coil changes, knife and roll setups are tracked as separate downtime reasons.
-
Weighing and scrap
Weights from scales and weighbridges are compared in an input-output balance, and edge trim, head/tail and scrap are calculated per work order.
-
Energy consumption
Electricity and natural gas use is measured per line, furnace and compressor, and energy per ton is reported.
-
Condition monitoring
Current, temperature and vibration on main motors, gearboxes and hydraulic units are watched to give maintenance early warning.
Processes we work on
Where the data starts in metal and steel
- Coil slitting lines
- Cut-to-length (CTL) lines
- Hot and cold rolling
- Welded tube and profile mills
- Wire drawing
- Heat treatment and annealing furnaces
- Galvanizing and coating lines
- Weighbridges and coil weighing
- Laser and plasma cutting
How a project runs
From discovery to live, step by step
- 01
Survey of lines and weighing points
Line PLCs, drives, scales and label printers are reviewed on site, and we decide where the coil number is read along the flow.
- 02
Pilot line
Data collection, downtime tracking and coil records go live on one slitting or cut-to-length line.
- 03
Energy and condition monitoring
Energy analyzers and sensors on critical equipment are added to the same data model.
- 04
ERP integration and rollout
Coil receipts, work orders and production confirmations are connected to the ERP, and further lines are added.
Built on Proxus
Proxus collects data from line PLCs, scales and energy analyzers at the edge, combines it with coil and work-order context and buffers it through network outages.
Proxus is the industrial data platform built by the VOLSOFT team.
Frequently asked questions
Common questions
How is coil tracking done on slitting and cut-to-length lines?
Coil tracking matches the input coil's number and weight with the resulting strips and bundles in one work-order record. Length and downtime come from the line PLC and weight from the scale. Each bundle's source and the scrap produced are then known from records.
Do rolling and tube mill PLCs need to be modified to collect data?
In most cases, no. Data is read from the existing PLCs and drives without changing control logic. If a missing signal is needed, the change is planned with the plant's automation team.
Can weighbridge and scale data feed the production system?
Yes. The communication outputs of scales and weighbridges are read and the weight is written to the coil, bundle and work order, so manual weigh tickets are no longer needed.
Why does energy monitoring matter in metal processing?
Rolling, heat treatment and furnaces use a lot of energy, so energy is a major cost line. Metering per line and per asset makes energy per ton and idle consumption visible and provides data for ISO 50001 work.
How long does a project take in a metal processing plant?
It depends on the number of lines, weighing points and the scope of the ERP integration. Projects usually start with a pilot on one line, and the scope is set during the discovery call.
Related pages
Often looked at together
- SolutionEnergy MonitoringMeter and analyzer data turned into energy per unit, EnPIs and ISO 50001 reporting.Explore→
- SolutionOEE SoftwareOEE software fed by PLC and CNC data, with downtime reasons, work orders and ERP sync.Explore→
- ServiceEdge ComputingProcessing close to the machine, buffering through outages and rules that run on site.Explore→
- SolutionPredictive MaintenanceCondition monitoring with vibration, temperature and current data, anomaly alerts and CMMS links.Explore→
- ServiceERP–MES IntegrationWork-order and production feedback integration with SAP, Dynamics and other ERPs.Explore→
- TechnologyHeidenhain CNC data collectionReading state, program and alarm data from Heidenhain TNC controls over LSV2.Explore→
Next step
Let’s turn your goal into a clear engineering scope.
Tell us about your plant, your machines and your goal. An integration engineer will set up a discovery call with you.