Skip to content

Industry

Production data, traceability and MES integration for automotive suppliers

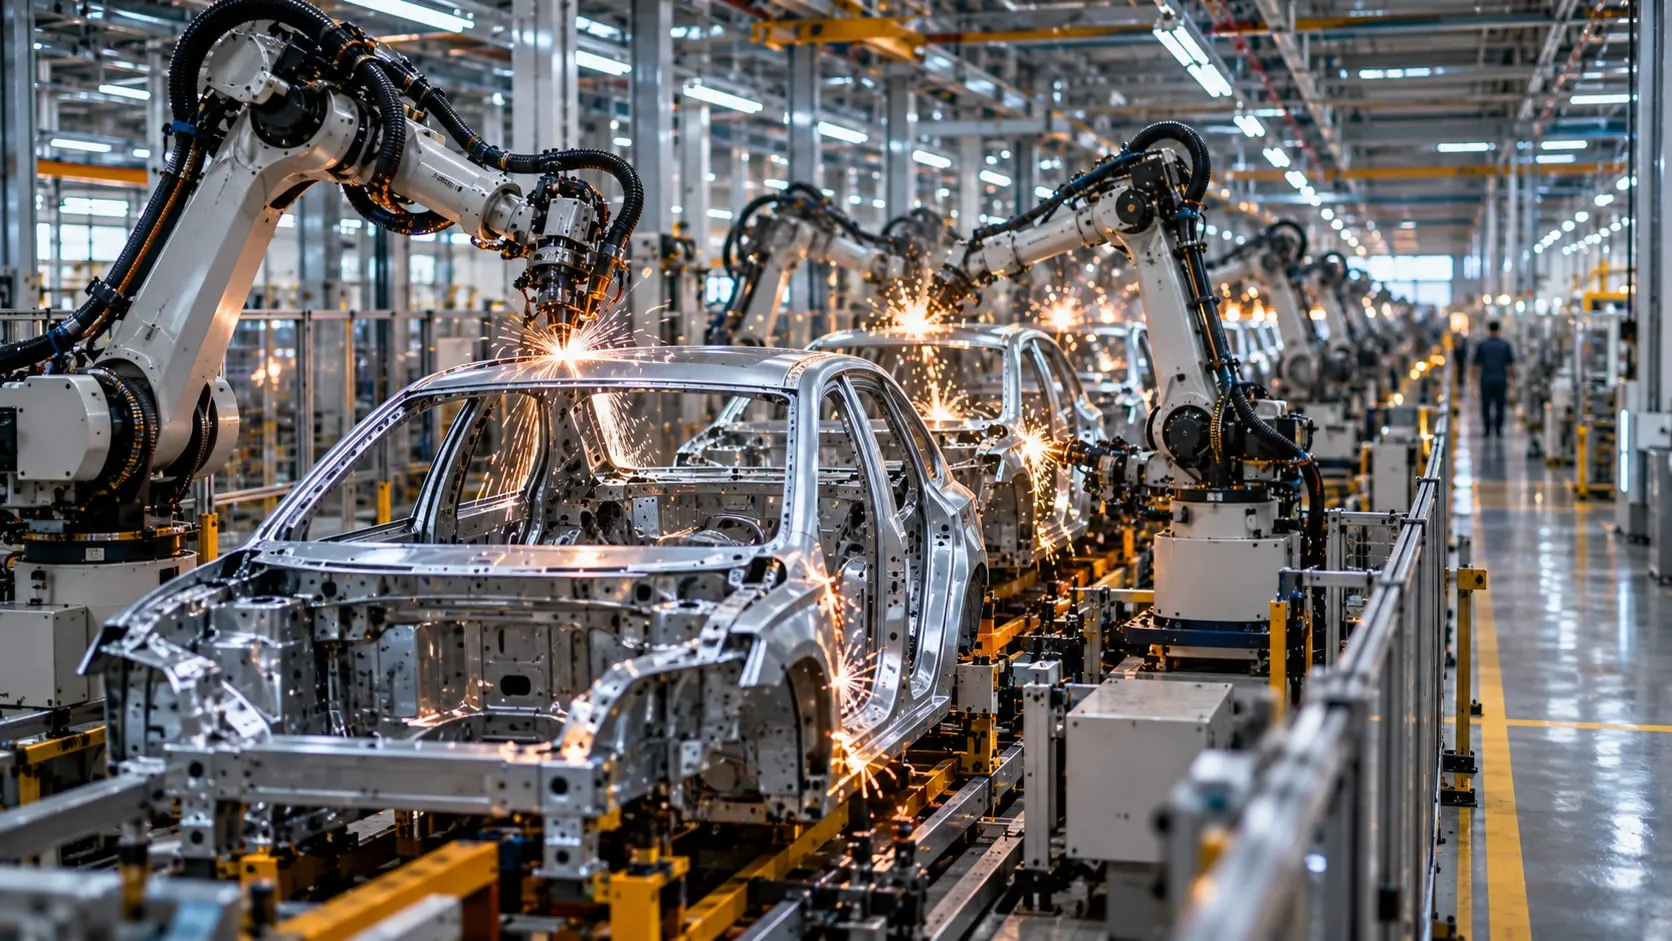
We take data from the PLCs and robots on press, welding, paint and assembly lines and bring part-level traceability, OEE and JIT/JIS call-offs into one data layer.

  • Siemens
  • Anadolu Isuzu
  • BSH
  • Tofaş
  • Toyotetsu
  • Martur
  • Turkcell
  • Vodafone
  • Doğadan
  • Pakmaya
  • Bross
  • Abdi İbrahim
  • Nobel İlaç
  • Plastimak
  • Dalgıç Kalıp
  • Barbaros Motor
  • Magneti Marelli
  • Rözmaş
  • Sanel

Automotive suppliers are asked for part and lot traceability, PPAP evidence and end-of-line test records, often during the same customer audit. In most plants that information is split between the press PLC, the welding robot controller, the paint line SCADA and spreadsheets filled in at the end of each shift.

VOLSOFT is a system integrator: we do not write PLC programs or build panels. We connect to existing controllers without touching their control logic, collect cycle time, downtime, counts and scrap along with process parameters such as weld current, tightening torque and oven temperature, and link them to the work order and the part serial number.

The result is one layer that shows the OEM's JIT/JIS call-offs, work orders and line data together, posts production confirmations to the ERP and answers a traceability query from recorded data. Every project runs on Proxus.
What we deliver

Automotive

  • Part and lot traceability

    Serial numbers, DMC/barcode reads and lot data are matched with the station, die, operator and process parameters each part saw. Backward and forward trace queries for an IATF 16949 audit are answered from recorded data.

  • Data from press, welding and paint lines

    We read cycle, downtime and alarm data from Siemens S7, Allen-Bradley, Mitsubishi and Omron PLCs and from KUKA and Yaskawa robots. On paint lines, oven temperatures and booth conditions are kept as process data.

  • OEE and downtime reasons

    Availability, performance and quality are calculated per line and per station. Downtime reasons are picked on the operator panel or assigned automatically from PLC alarms.

  • JIT/JIS call-offs and work orders

    Sequenced call-offs from the OEM and ERP work orders are shown on the line screen. Good count, scrap and shipments are posted back to the ERP automatically.

  • Tightening and end-of-line test records

    Torque and angle values, leak and functional test results are stored against the part serial number, so a nonconforming part's history is one query away.

Processes we work on

Where the data starts in automotive

  • Sheet metal press lines
  • Robotic spot and MIG welding cells
  • Paint lines and curing ovens
  • Interior trim injection molding
  • CNC machining
  • Bolt tightening stations
  • Assembly lines and poka-yoke
  • End-of-line leak and functional testing
  • JIT/JIS sequenced shipping

How a project runs

From discovery to live, step by step

  1. 01

    Site survey and line inventory

    We review the PLCs, robots and test stations on each line, existing barcode/DMC points and the ERP work-order flow on site. Together we decide which data is captured at which station for traceability.

  2. 02

    Pilot line

    Data collection, downtime tracking and part records usually go live on one press or welding line first. The data model and naming are settled there.

  3. 03

    ERP and JIT/JIS integration

    Work orders, materials and production confirmations are connected to the ERP, and sequenced call-offs to the OEM interface. The new flow runs in parallel until the existing process can be switched.

  4. 04

    Rollout and training

    Further lines are added with the same data model. Operators, shift leads, quality and maintenance are trained on their own screens.

Built on Proxus

Proxus collects data from PLCs, robots and test stations on the shop floor, buffers it if the network drops and passes it to the ERP and reporting layer with part, work-order and line context. It runs on the plant's own servers.

Proxus is the industrial data platform built by the VOLSOFT team.

OT/IT integration with Proxus ↗

From the field

One of the clients we work with in this industry

References →
Anadolu Isuzu

Data collection from production equipment and energy systems

Data was collected from production equipment and energy systems. The client reached level 3 in the SIRI Industry 4.0 maturity assessment.

“Their flexibility is impressive in the workflow.”

Aşkın İnci · CIO, Anadolu Isuzu

Source: the client’s review on Clutch

Frequently asked questions

Common questions

How do automotive suppliers achieve traceability?

Traceability comes from automatically recording which station, die, parameters and operator each part or lot went through. Barcode/DMC reads, PLC data and the work order are combined in one data model. Those records answer backward and forward trace queries during an IATF 16949 audit.

Do we have to change PLC programs on press and welding lines to collect data?

Usually not. Data is read from the existing PLCs without changing their control logic. If a needed signal does not exist in the PLC, the change is planned with the plant's own automation team or contractor.

What automotive work has VOLSOFT done?

At Anadolu Isuzu, data was collected from production equipment and energy systems. According to the client's review on Clutch, the company reached level 3 in the SIRI Industry 4.0 maturity assessment.

Can JIT/JIS call-offs feed the production monitoring system?

Yes. Sequenced call-offs from the OEM can be taken from the ERP or EDI interface and shown on the line screen and in the work-order queue. Produced and shipped parts are matched to the same record.

How long does a production monitoring rollout take in an automotive plant?

It depends on the number of lines and machines, the traceability scope and how deep the ERP integration goes. Projects typically start with one pilot line, and the scope is set during the discovery call.

Next step

Let’s turn your goal into a clear engineering scope.

Tell us about your plant, your machines and your goal. An integration engineer will set up a discovery call with you.

Awards and references

The integration team manufacturers trust

See our references →